Define the fault
Agree the pack, line speed, critical seal area and pass/fail tolerance.
Inspect heat seals, tray film, pouch seals, tamper features and closures—then reject failed packs automatically against your programmed criteria.
Inline seal integrity inspection can check every presented pack at production speed, reducing the gaps left by periodic manual sampling.
Oxford Vision Systems combines product handling, visible-light cameras, thermal imaging or other suitable sensing, software and reject controls into one production-ready inspection point. The system is designed around your real packs, expected defects and acceptable process variation.
Vision, thermal inspection and leak testing answer different quality questions. We help define which method—or combination—provides evidence for the failure modes you need to control.
Read the seal inspection method guide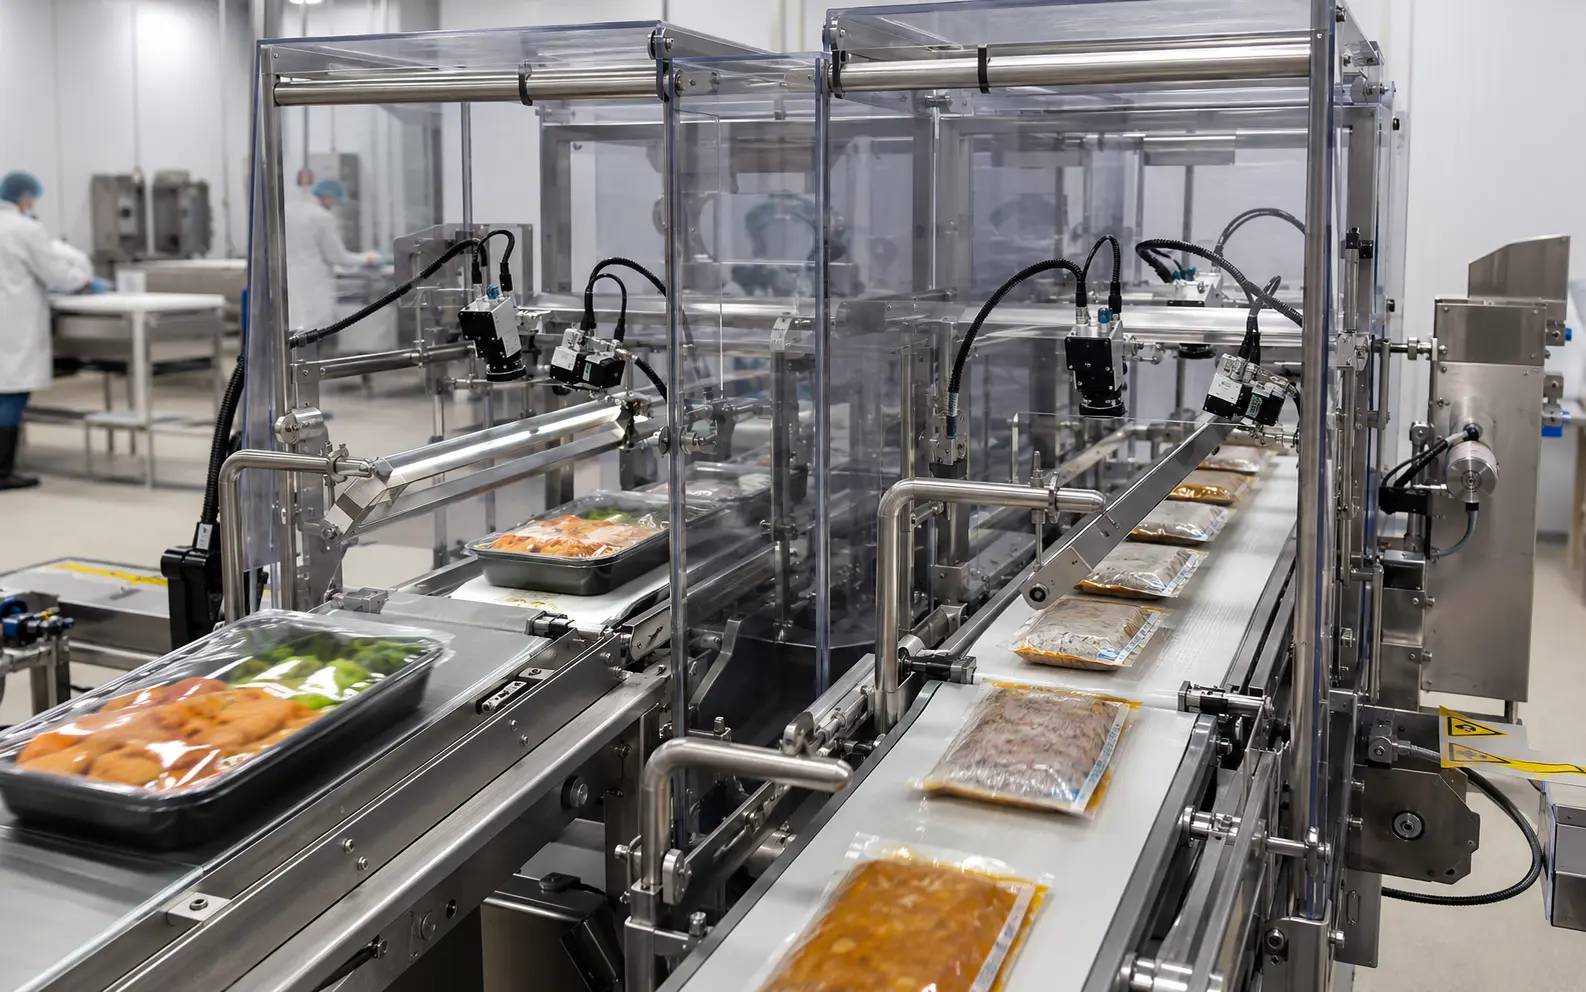
Purpose-designed lighting reveals the critical seal edge. Image processing separates true faults from film texture, artwork movement and acceptable production variation.
Choose a focused station or combine several inspections where line access, resolution and cycle time permit.
Detect incomplete, inconsistent and visibly failed seal regions.
Explore systemCheck lidding-film presence, position, folds and perimeter defects.
Explore systemInspect top, side and end seals on flexible packs and sachets.
Explore systemIdentify visible product, powder, liquid or particles in the seal path.
Explore systemVerify bands, membranes and required tamper features are present.
Explore systemUse suitable vision, sensing or thermal methods to confirm foil presence.
Explore systemFind missing, high, skewed, damaged or incorrect closures.
Explore systemTrack and remove failed packs with confirmation and fail-safe monitoring.
Explore systemReliable inspection begins with realistic defects and finishes with the line proving that the correct failed pack was removed.
Agree the pack, line speed, critical seal area and pass/fail tolerance.
Trial representative good packs, known failures and normal production variation.
Specify handling, optics, lighting, controls, guarding and reject method.
Install, commission and test the complete inspection and rejection sequence.
Inspection performance depends on stable product presentation, controlled lighting, precise tracking and a reject sequence designed for the pack.
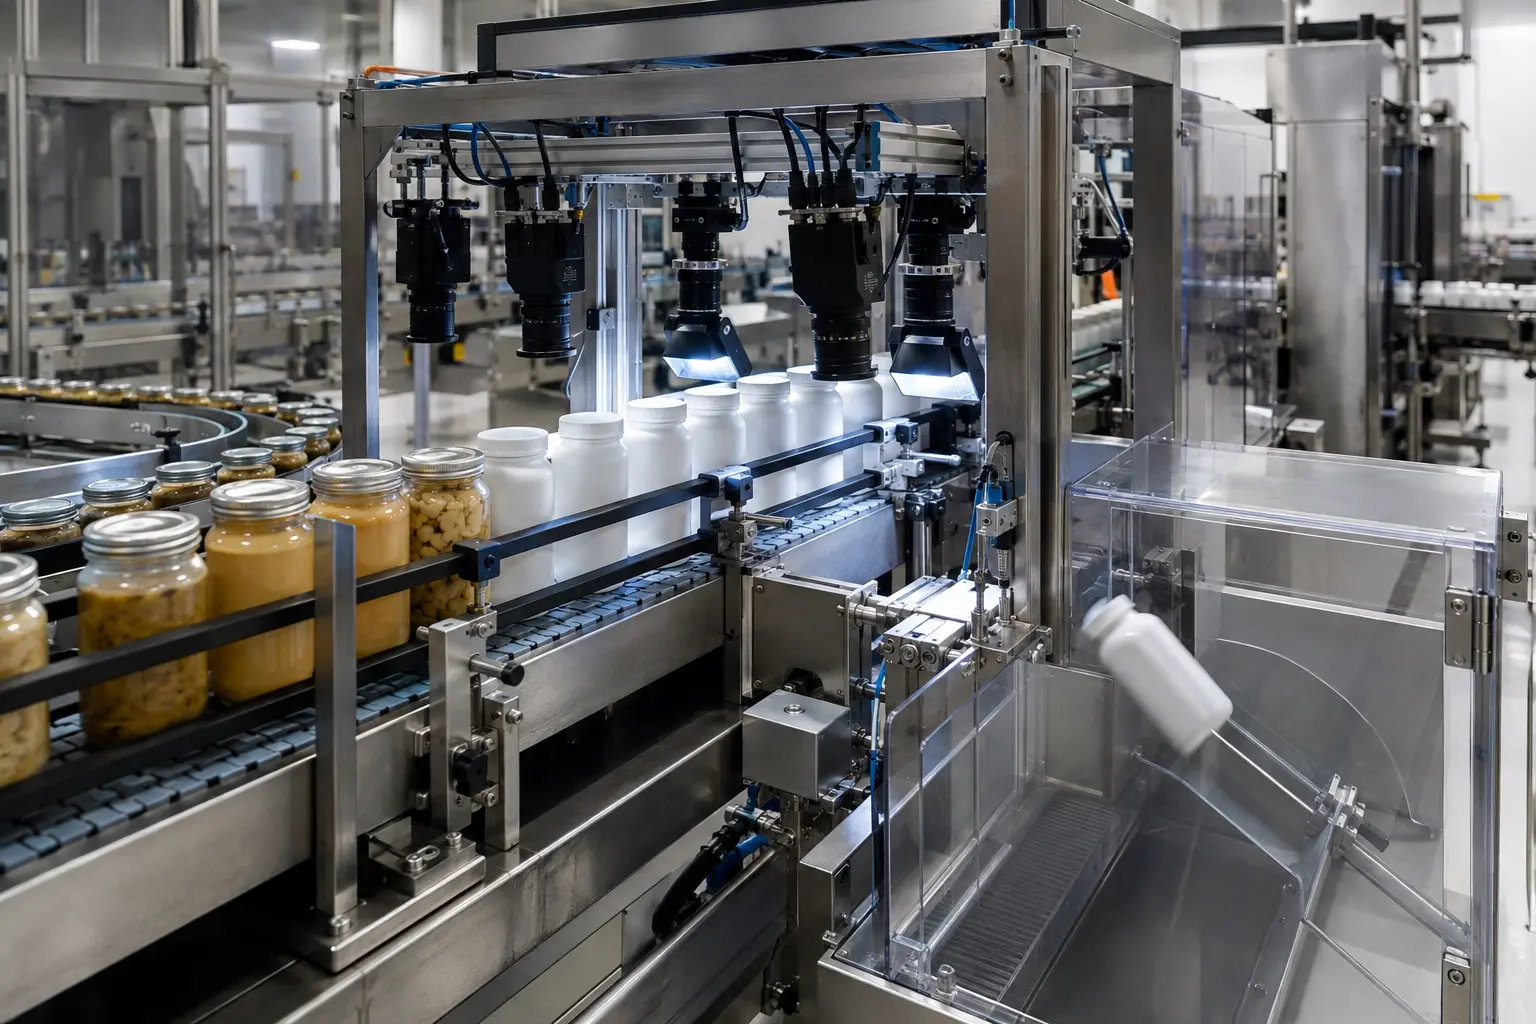
Hygienic, guarded and line-integrated solutions for food, beverage, pharmaceutical, healthcare, cosmetics, chemical and general manufacturing applications.
Our practical guide compares machine vision, thermal seal inspection and leak testing. It maps common packaging faults to suitable methods and covers MAP/CAP packs, 100% inspection, retrofit surveys, validation, data and reject verification.
Read the seal inspection guideLabel each trial pack with the question it is intended to test. A visible fold, an abnormal thermal pattern and a known integrity failure are useful examples for different purposes; do not assume that every method should respond to every example in the same way.
Record format, film or tray identity, product condition, fault location and the responsible team’s classification. Include accepted packs close to the visual boundary as well as clear faults. Where a separate test establishes a property, retain that result and its method with the sample record instead of inferring it from appearance.
A reference image remains a record of one observation, while a physical pack may change as it cools, dries, deforms or is handled. State the condition and inspection timing used for the comparison. Replace or reclassify an altered sample through the agreed quality process rather than treating it as an unchanged reference indefinitely.
Include the permitted pack orientation, spacing and speed changes. Test a required seal region that is hidden or outside the view, and record an unavailable inspection separately from a passed check. Keep the pack reference associated with the downstream reject or hold action.
After a change to lighting, recipe or presentation, challenge both the known faults and the accepted boundary samples. Record which result improved and whether another result worsened. The seal defect guide and acceptance checklist provide routes for agreeing the sample classes and production evidence.
Clear answers before you invest in an in-line inspection project.
Systems can be engineered for heat seals, tray lidding film, pouch and sachet seals, tamper-evident features, induction-foil presence and cap or closure integrity.
Yes. We can integrate a reject mechanism, product tracking, confirmation sensing and fail-safe monitoring around the pack and line requirements.
Most projects can be integrated with an existing conveyor or packaging machine, subject to a site survey covering access, presentation, line controls, guarding and available space.
We start with representative good packs, known failures and normal production variation. Trials establish the sensing method, image quality and realistic acceptance criteria before final engineering.
Yes, where specified. Options include fault images, production counts, fault categories, recipe records and connections to line or factory data systems.
AI can help when acceptable packs and genuine defects vary in appearance or fixed rules become too complex. It should be selected only when representative trials show a practical improvement.
Cost is shaped by the defect, pack range, line speed, lanes, sensing method, handling, reject controls, data, guarding, installation and acceptance requirements.
A visible seal fault, an abnormal temperature pattern and a leaking finished pack are different observations. Choose the method from the required decision and prove its limits on the actual packaging.
Assess camera access and contrast for the specific seal region. A transparent film, printed film and reflective pack may need different imaging arrangements. Use the defect guide to organise labelled samples, including acceptable variation and marginal faults.
A thermal inspection examines the heat pattern under the agreed process conditions. Trial the timing and presentation with real packs and production variation. The thermal inspection guide explains why this evidence must not automatically be described as a leak or seal-strength result.
Specify the leak-test question and acceptance method separately from appearance checks. Some projects need complementary methods. Use the seal-integrity testing guide with the responsible packaging team to define what each result can establish.
Define the response when a pack is missing from the expected view, a region is obscured or the inspection cannot decide. Treat invalid results explicitly and prove that the correct pack follows the required reject or hold route.
Record sample identity, fault category, format, speed, viewing coverage and result. Separate missed faults from rejected good packs and include the complete reject sequence. The acceptance checklist helps turn an attractive demonstration into a documented project decision.
Tell us the pack format, line speed and seal fault you need to detect. We’ll review the application with you.